Construction & Building presses
6 presses
Most jobs start with the tool dimensions; the plate or profile size and the daily quantity are enough.
Parts pressed in this sector
Some of these are genuine samples pressed on ÖZKOÇ presses; the ones marked representative show only the shape of the part. If you find one that resembles your own part, send us its drawing and we will tell you which press it is made on. Send your part drawing

Seamless pipe tee and elbow fitting 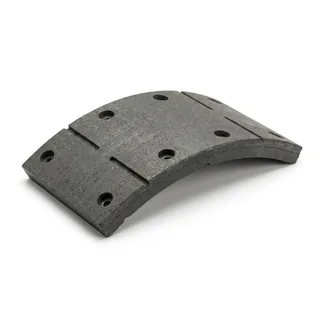 representative
Heavy-duty friction element 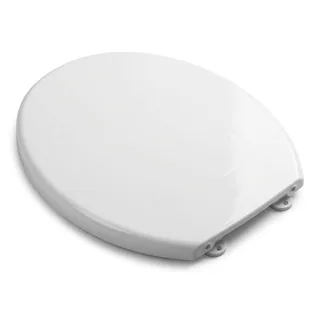 representative
Composite sanitary product and household item  representative
Melamine-faced surface panel 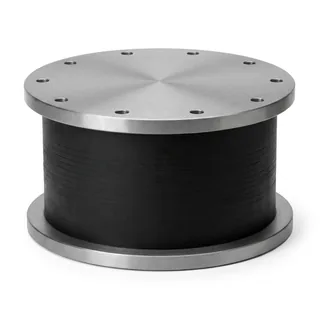 representative
Rubber seismic isolator  representative
Elastomeric bearing 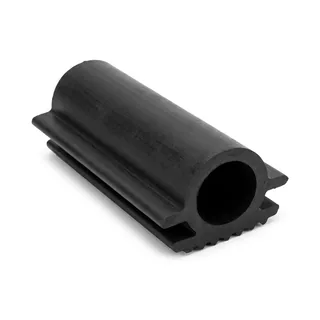 representative
Building expansion joint and sealing profile  representative
Airport and façade sheet metal cladding panel 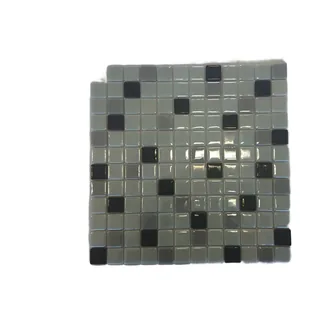
Glass mosaic tile  representative
Ceramic border and decorative moulding
Presses used in this sector
 COLD
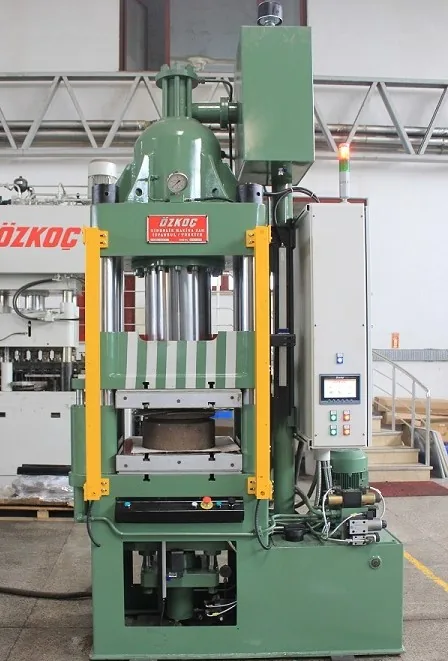
Hydroforming Press (T-Fitting Press)
Hydroforming (T-fitting) press — a hydraulic press that forms weld-free, seamless T-fittings by applying fluid pressure inside a tube.
- Plumbing tees and elbow fittings
- Pipe fittings
- Sanitary plumbing parts
 HOT
Brake Lining Curing Press
A hydraulic press that cures the resin-based friction compound of brake linings under pressure in a heated mould.
- Earthmoving machine and crane brake linings
- Heavy-duty friction elements
 HOT
Melamine Press
A hot hydraulic press that presses tableware, panels and sanitary products by curing melamine and resin-based thermoset compounds in a heated mould.
- Toilet seats and sanitary products
- Melamine-faced surface panels
- Decorative laminate elements
 HOT
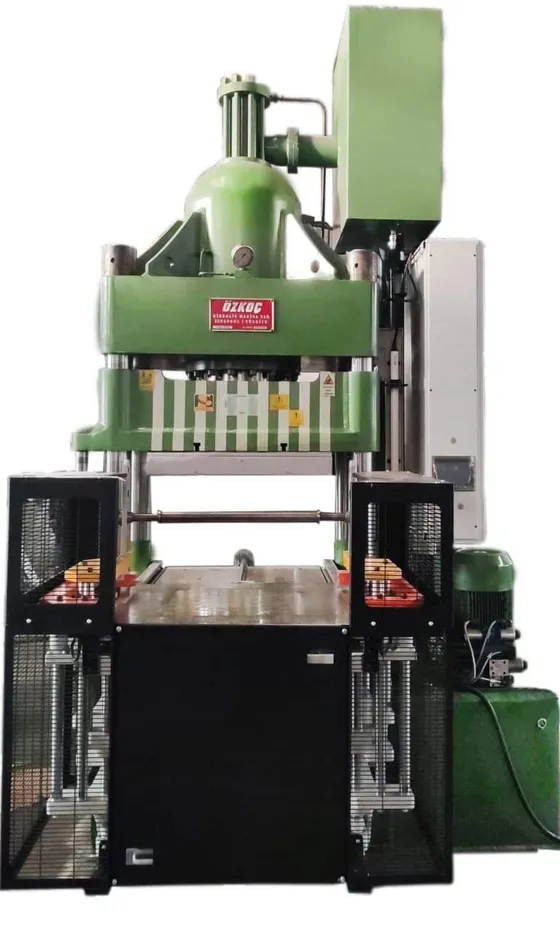
Rubber Curing Press
A hydraulic press that vulcanises rubber compound under pressure in a heated mould; on metal-reinforced parts the bond is formed in the same cycle.
- Rubber seismic isolators
- Elastomeric bearings
- Building expansion joint and sealing profiles
 COLD
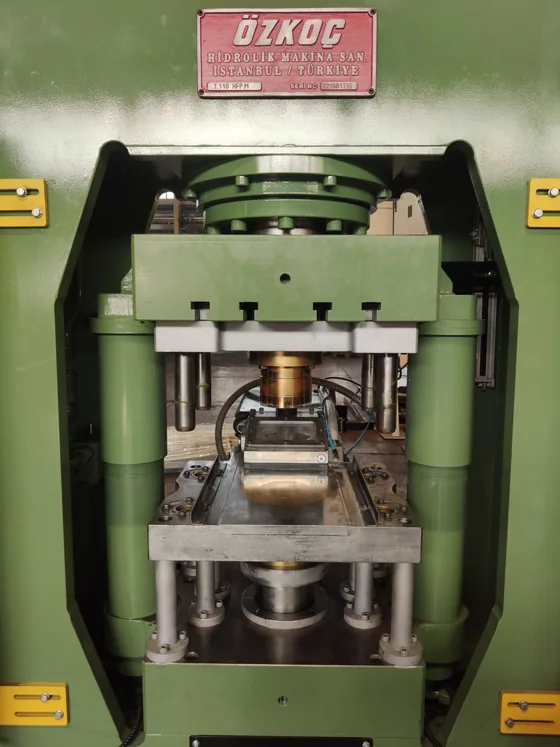
Deep Drawing Press
Deep drawing press — draws sheet metal into seamless vessel and body forms; the blank holder prevents wrinkling, and blank holder force and drawing speed are set independently.
- Airport and façade sheet metal cladding panels
 SPECIAL
Powder Compacting Press
Powder compacting press — compacts dry powder and granulate blends in a die and turns them into green parts for the kiln; salt cores, zirconia blocks and glass mosaics are pressed in the same class of machine.
- Glass mosaic tiles
- Pool and façade mosaics
- Decorative cladding elements
What matters when choosing a press?
Hydroforming Press (T-Fitting Press)
- Tube in, T outIt does not join separate parts; it produces the finished fitting from a single tube in a single cycle.
- Weld-free, seamless fittingA weld seam is the weak point for both sealing and fatigue; here there is no joint at all.
- Axial feeding under matched controlInternal pressure and end feeding are set together; wall thinning stays under control.
- Short cycle timeAgainst cheap equivalents, the purchasing decision is made by output per hour.
Brake Lining Curing Press
- Degassing cycleGas forms during curing; if it is not vented the part blisters and the friction surface stays porous.
- Zoned mould heatingA temperature difference across the mould shifts the friction coefficient from part to part.
- Top-acting, bottom-acting and multi-daylight frame arrangements
Melamine Press
- Thermoset curing, no way backA cured part cannot be remelted; quality is determined not by force but by thermal discipline.
- Zoned heating and degassingIf the volatiles formed in the compound are not vented, blisters and porosity are left on the surface.
- Two-daylight toilet seat arrangementOn a large, asymmetric seat a ram that descends parallel holds thickness and flatness.
- The same hot press family as the silicone and rubber presses
Rubber Curing Press
- Vulcanisation under pressureThe material that enters the mould as a dough leaves it as an elastic part.
- Metal and rubber togetherThe metal insert is placed in the mould and the rubber is cured onto it; the bond needs no separate station.
- Large-area plate, bearing and profile work
Deep Drawing Press
- Adjustable speed and blank holder forceDrawing speed and counter-holding force are set to suit the part in order to keep wrinkling under control. As the sheet gains depth, material builds up at the edge; the blank holder holds it down and eliminates wrinkling.
- Blank holder pressure is decisiveIf the pressure is too low the sheet wrinkles, if it is too high the flow is choked and the part tears; the window between them is narrow.
- Seamless vessels and bodies, multi-stage drawing
Powder Compacting Press
- Dry powder, compacted in the dieThe powder fills the die cavity and interlocks under pressure; the part comes out hard enough to be handled.
- Even density at every pointA difference in density changes shrinkage in the kiln locally; distortion and cracking arise from this.
- Staged pressure, ramped releaseTrapped air that is not vented raises blisters; if the pressure is released suddenly the green body cracks.
- The same principle, different automationSalt cores, zirconia blocks and glass mosaics are the same compaction; what changes is the die and the feeding.