Rubber Curing Press
- Vulcanisation under pressureThe material that enters the mould as a dough leaves it as an elastic part.
- Metal and rubber togetherThe metal insert is placed in the mould and the rubber is cured onto it; the bond needs no separate station.
- Large-area plate, bearing and profile work
What is a Rubber Curing Press?
The rubber curing press vulcanises rubber compound under pressure in a heated mould: the material that enters the mould as a plastic dough leaves it as an elastic part. The press's job is to keep temperature, pressure and time stable.
On parts where metal and rubber are processed together the bond is formed in the same cycle. When the cycle ends is dictated not by the speed of the press but by the chemistry of the cure; a part opened too early stays undercured, one opened too late turns brittle.
Is this press right for you?
Suitable
- Technical rubber parts vulcanised in a mould
- Large elastomeric bearing pads used in bridge and building connections
- Metal-reinforced vibration isolation mounts and bushings
- Wide-section expansion joint and sealing profiles
- If your material is silicone: Silicone Curing Press
- If you will press friction linings: Brake Lining Curing Press
Construction & Building — parts typically produced in this sector
These images are representative — they show the shape of the part; they are not the exact parts we produce. If you find one that resembles your own part, send us its drawing and we will tell you which press it is made on. Send your part drawing
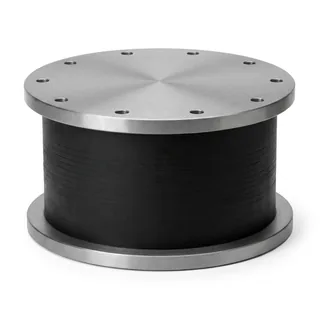 representative
Rubber seismic isolator  representative
Elastomeric bearing 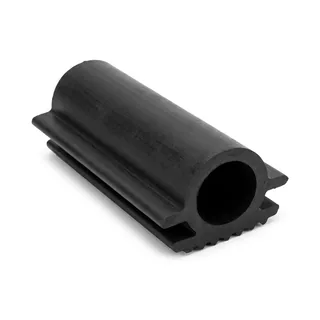 representative
Building expansion joint and sealing profile
Automotive — parts typically produced in this sector
 representative
Elastomer mount and vibration isolation element 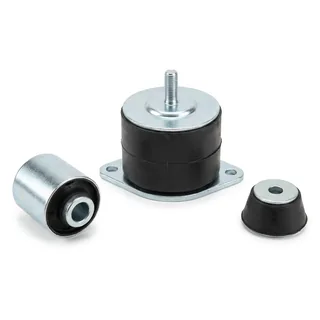 representative
Rubber-to-metal bonded mount and bushing
This press at work
Tap the cover and the video opens on this page. Until you do, no request goes to YouTube.
Özkoç 400 tonne Hydraulic Rubber Vulcanising Press
For those who want the detail
How vulcanisation proceeds and where the metal-to-rubber bond is formed
Rubber compound enters the mould as a plastic dough. Under heat and pressure the material becomes an elastic part that cannot go back. The press's task is to hold temperature, pressure and closing position steady throughout that period.
It is not the press that decides when the cycle ends but the cure curve of the compound. A mould opened too early yields an undercured part, one opened too late a brittle one. Cure time is therefore tied to the HMI recipe, the mould is heated zone by zone, and thermocouple feedback closes the temperature difference across the platen.
On parts where metal and rubber are processed together the press does two jobs in one cycle: the metal insert is placed in the mould, the rubber is cured onto it and the bond is formed in the mould. Vibration mounts, bushings and bearings are produced this way; no separate bonding station is needed.
On large-area work — such as the big elastomeric bearing pads used in bridge and building connections — what is decisive is that pressure is distributed evenly across the plate. On parts like these, where the load falls off centre, the rigidity of the frame and a ram that descends parallel directly determine the thickness tolerance.
For small parts in high volumes a rubber injection moulding machine is faster. This press is the machine for medium batches and large-area parts; it comes from the same hot press family as the silicone and melamine presses, and what changes is the mould and the recipe.
- Zoned platen heating with thermocouple feedback
- The cure recipe is managed from the HMI and the cycle follows the recipe
- Adjustable degassing (breathing) steps
- On metal-reinforced parts the bond is formed in the same cycle
- A frame arrangement suited to large-platen plate and bearing work
Rigid frame joined with prepared weld bevels
When the form or the embossing does not come out, the toolmaker is blamed straight away. More often than not the die is not the cause: the press frame deflects under load and the two halves of the die no longer seat fully on each other. The share the frame has in this is usually unknown on the buyer's side, because it is written in no catalogue.
When ÖZKOÇ builds the frame as a welded construction, it joins the crossbeams and the plates BY PREPARING A WELD BEVEL. There are many companies in the sector that join without preparing a bevel; the weld then stays on the surface only. Once the bevel is prepared, the weld penetrates the cross-section and the frame resists deflection under load.
This holds for every frame type, monoblock or column-type — it is not an option that depends on the type of press, it is ÖZKOÇ's manufacturing discipline.
- Crossbeams and support plates are joined with a prepared weld bevel.
- The weld does not stay on the surface, it penetrates the cross-section; the frame does not deflect under load.
- The same discipline is applied whether the frame is monoblock or column-type.
Ram parallelism system
On wide and asymmetric parts the load bears on one corner of the ram; the ram comes down slightly tilted and one corner of the part turns out thicker than the other. The result: excess material, uneven strength, unnecessary heat and cycle time.
In the ram parallelism system designed by ÖZKOÇ itself, four counter-pressure cylinders bring the ram down parallel to the lower plate. The difference in thickness between the corners drops to a minimum; material is saved, and the homogeneity of the part keeps the strength where it is wanted.
The same arrangement works in cutting as well: at the instant the shear occurs, the counter-pressure cylinders absorb the shock, maintain parallelism and extend the life of the cutting die.
- Four counter-pressure cylinders bring the ram down parallel to the lower plate.
- On a wide and asymmetric part the difference in thickness between the corners drops to a minimum.
- Material savings + homogeneous strength.
- In cutting it absorbs the shock and extends die life.